Missing Labels on a Roll: Count Empty Positions Separately from Quantity
A web position is not always a usable printed label
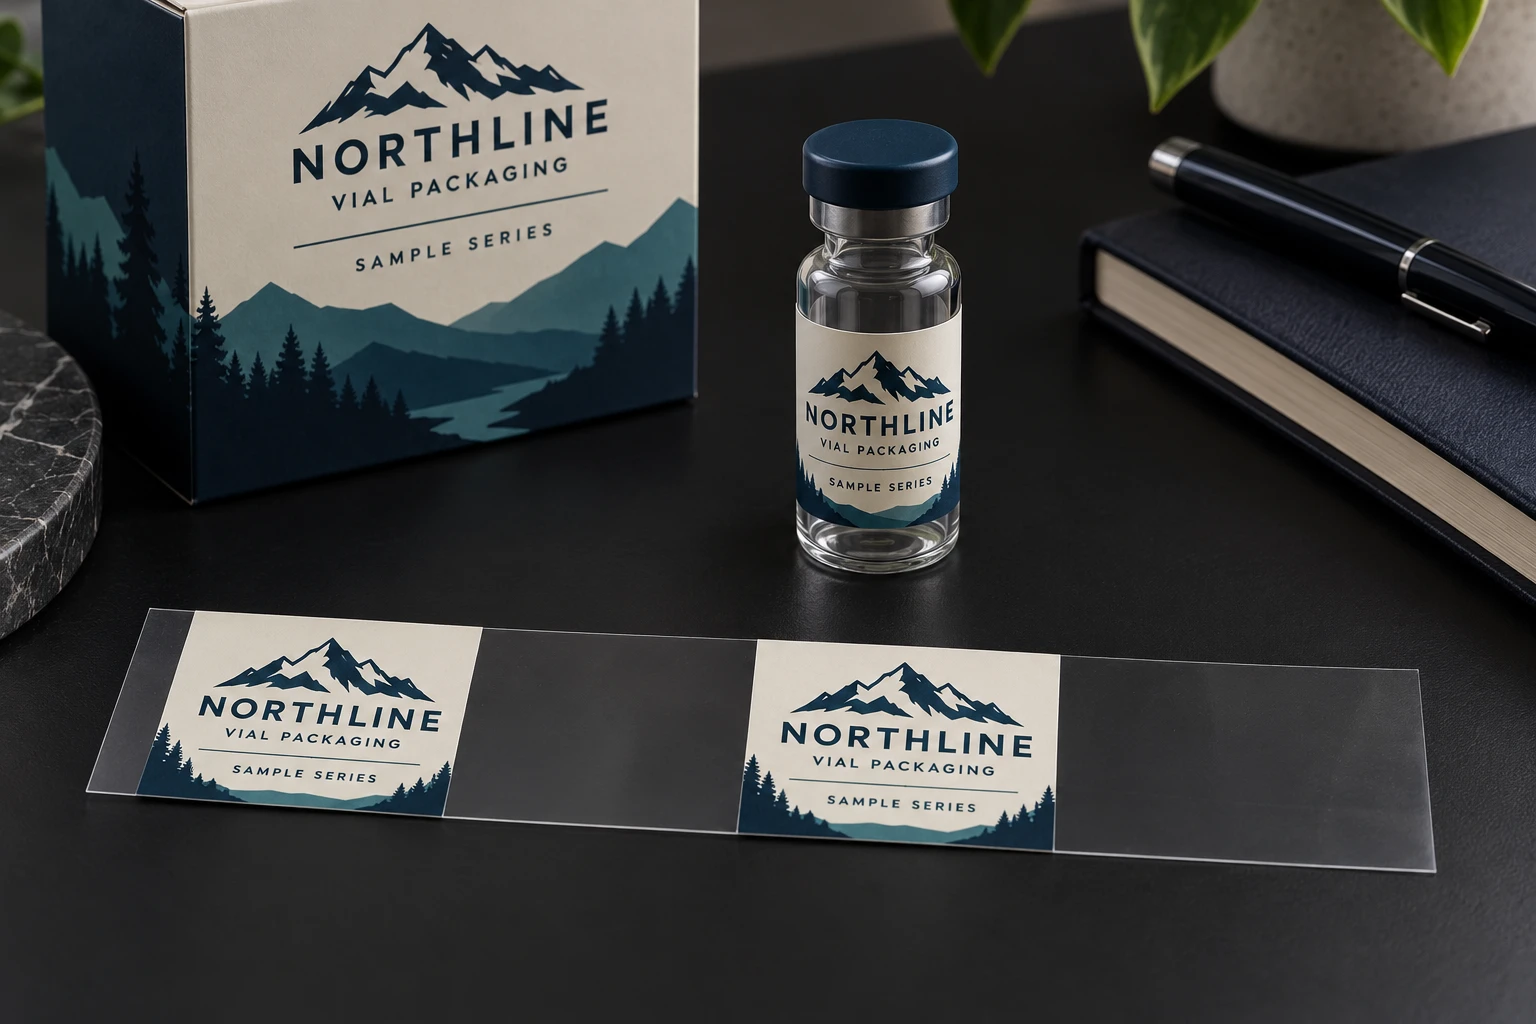
A roll may contain regularly spaced positions with no label on the liner. The purchasing problem is not resolved by saying the roll has the expected length or that the counter reached a number. The buyer needs to know how many usable labels were supplied and whether empty positions affect the packer’s process.
Start by documenting the empty positions and checking the counting basis in the quotation. Do not assume every empty space is an error, a splice or an allowed setup section. Its location and the agreed delivery terms determine the next question.
Locate the empty positions before explaining them
Record the roll identity and whether the empty positions occur at the beginning, end, near an identified join or among printed labels. Photograph enough continuous web to show the relationship. A tight image of bare liner cannot distinguish an intentional leader from missing labels in the usable run.
If the roll has already been used, state how much of it was observed and how the observation was made. Preserve an unused example where possible. Do not report a whole-roll count based on the few positions visible in a photograph.
Ask the supplier whether the delivered quantity excludes blank positions and how the roll’s quantity label was determined. The answer should identify the agreed unit and method. “Pieces” is useful only when both sides mean usable printed labels rather than web repeats or a nominal machine count.
Keep three quantities in the record
The ordered quantity, delivered declared quantity and inspected usable quantity answer different questions. There may also be an estimated remaining quantity, which should be clearly marked as an estimate. Combining these figures makes a shortage complaint harder to resolve.
| Record | What it should mean | Common ambiguity to remove |
|---|---|---|
| Ordered labels | Quantity requested for each approved design | Total across all designs versus per design |
| Declared delivered labels | Supplier’s stated usable-label quantity and counting basis | Whether blanks or setup web were included |
| Observed empty positions | Identified locations and actual inspection scope | Extrapolation from a short section to the entire roll |
| Accepted usable labels | Quantity assessed under the agreed method | Treating all visible labels as accepted without review |
| Remaining unknown stock | Portion not yet assessed | Presenting an estimate as a confirmed shortage |
A quantity tolerance, if agreed, does not automatically authorize interruptions wherever they occur. Conversely, a packer’s difficulty with empty positions does not alone prove a numerical shortage. Quantity conformity and presentation compatibility need separate decisions.
Ask how the packer handles a gap in supply
The packer should identify whether empty label positions can be detected and managed within the agreed process. Do not prescribe a sensor setting or assume every line behaves the same way. State whether the affected positions are identified and whether the supplier proposes a delivery arrangement the packer can accept.
If the concern is a splice, refer to the actual splice agreement. If it is an intentional leader or trailer, identify that section separately. These features may all involve bare liner, but their purpose, location and counting treatment differ.
For custom vial label purchasing, ask the supplier to acknowledge the finished roll requirements and quantity basis before final release. A quotation for a total piece count leaves operational details unresolved if a contract packer has specific continuity requirements.
Two illustrative order reviews
In one example, a buyer orders a defined quantity per SKU and finds two empty positions inside a short inspected section. The supplier’s declared quantity is based on finished printed labels, and the buyer has not yet counted the roll. The immediate task is to verify the count and ask whether the presentation meets the packer’s requirements. Declaring a two-label shortage from those observations alone would assume a counting method that has not been established.
In another example, a supplier confirms that its stated number came from web repeats that included empty positions. The buyer’s order specified usable printed labels. Now the unit mismatch is central to the quantity discussion. The buyer should reconcile the actual usable count and agreed remedy rather than argue only about the appearance of the roll.
These are illustrative cases. They do not establish an acceptable number of missing positions or a universal counting standard. The purchase agreement and actual inspection determine the commercial outcome.
Make the correction traceable
When requesting replacement or supplementary stock, reference the original design and approved revision. Identify the quantity still needed under the agreed counting basis. If the supplier proposes inspection, ask which rolls will be checked and how the results will be recorded.
Do not let a supplementary quantity obscure a continuing presentation problem. A packer that cannot handle unmarked empty positions may need a different delivery arrangement even when the total usable quantity is sufficient. The replacement review should address both issues where both remain open.
Retain the original observations and the final reconciliation. This helps the next order use a clearer specification instead of repeating a dispute over what the word “quantity” included. It also prevents an estimated shortage from becoming an unsupported permanent claim about the supplier’s accuracy.
Frequently asked questions
Are empty positions always manufacturing defects?
Not necessarily. Some bare web may be intentional and agreed. Identify its location and purpose, then compare it with the finished delivery specification. Unexplained gaps within the usable run deserve a specific review.
Does the roll length prove the label count?
It may support a calculation only when pitch, lane count and the treatment of non-label sections are known. It does not independently establish usable printed quantity. Agree the counting basis with the supplier.
Should the packer simply ignore the gaps?
Only the responsible packer can assess compatibility with its process. Record its requirement and obtain an agreed delivery arrangement. Do not assume an equipment or workflow change is costless or appropriate.
If bare positions occur near a web join, the splice-policy guide helps check the separately agreed treatment of splices rather than counting every gap as the same feature.
Submit the count and presentation questions together
For a focused procurement review, send the quantity per design, roll references, declared counts, photographs showing the empty positions in context and the actual inspection scope. Include the packer’s continuity requirements. Ask for a clear distinction between usable-label count and web presentation before agreeing the next supply.